Author: Site Editor Publish Time: 2025-08-05 Origin: Site
Last updated: October 17, 2026
An industrial infrared oven project needs a defined process result, not only a heater rating. The product must reach the required condition at the agreed production rate, while its appearance, dimensions and other acceptance characteristics remain within the project's limits. A quoted turnkey scope should identify who will design, integrate, test and document that result.
The useful starting point is a linked record of product requirements, machine conditions and acceptance evidence. This keeps a successful sample trial from being mistaken for approval of every product, line speed or installation.
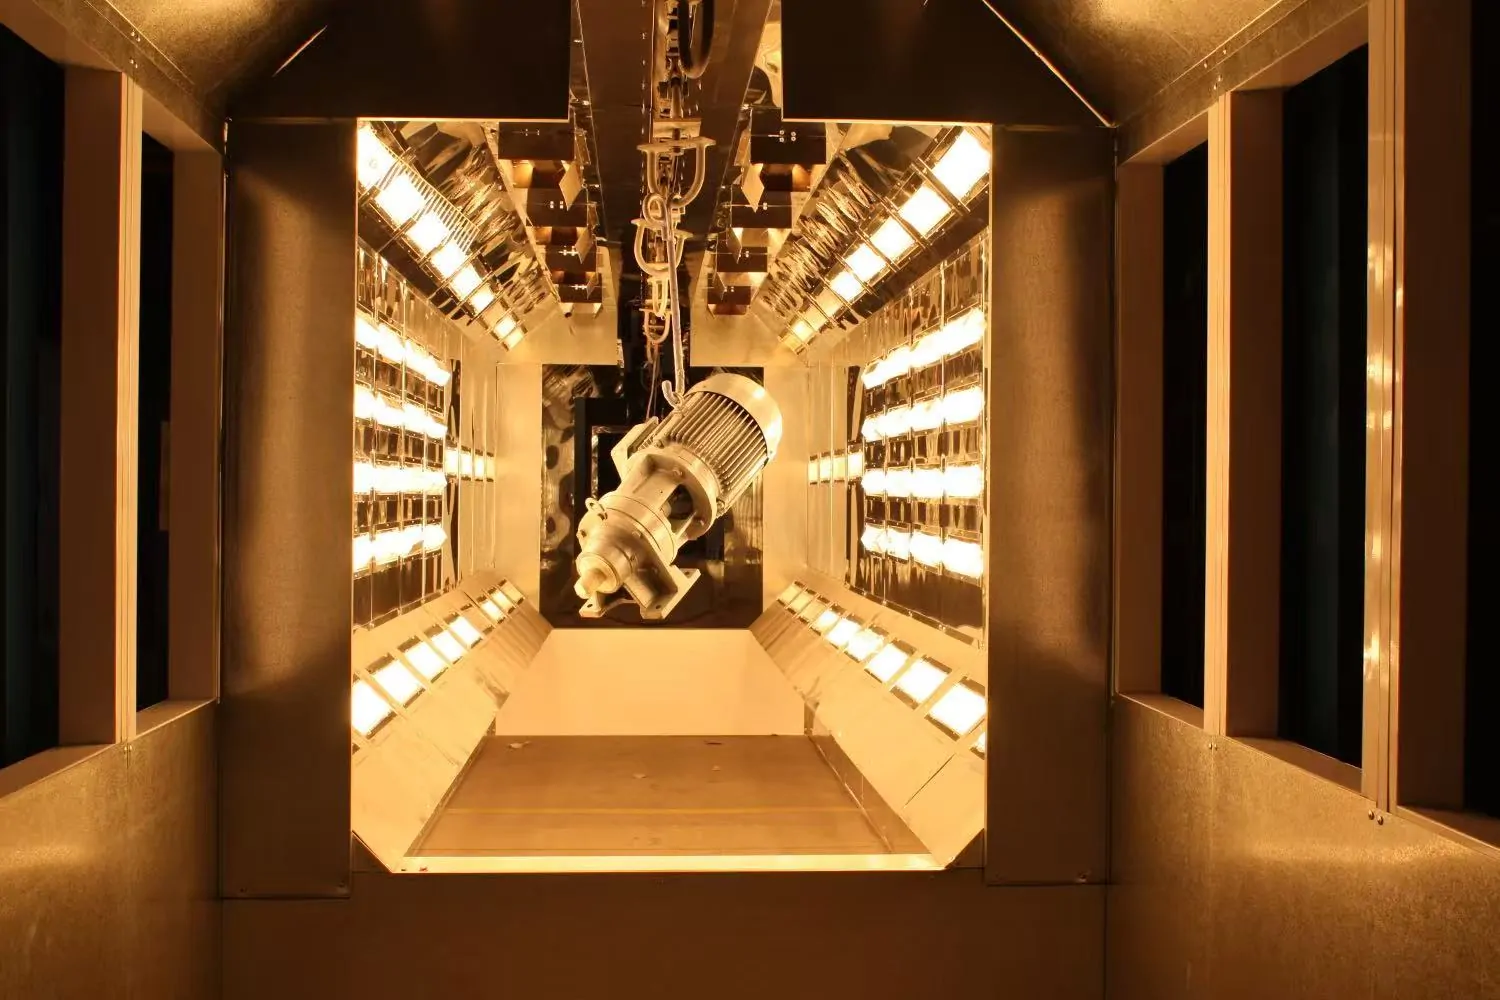
Keep the project’s process inputs together: material and coating, part shape and dimensions, load or conveyor arrangement, incoming condition, target output and available heating time. Identify which surfaces must be heated and which areas must be protected. Include variations that matter, such as a different coating, product mass or loading pattern.
Separate the thermal target from the finished-product requirement. A temperature profile may be an input to curing, bonding, drying or forming, but it does not by itself prove the required adhesion, moisture condition, appearance or dimensional result. Ask the relevant material or process owner to define the endpoint and its test method.
Write down the conditions the proposed equipment must cover. A trial on a simple, evenly loaded part does not establish performance on a heavier product, a hidden surface or a different conveyor loading pattern.
Absorbed radiant energy heats the exposed material; surface response and the time available for heat conduction affect the resulting temperature profile. For hidden surfaces or deeper thermal targets, evaluate conduction paths and a proposed infrared–convection combination against the actual part requirements.
The DOE Process Heating Sourcebook treats emitter selection, reflectors, controls and application testing as connected decisions. It also identifies uneven heating and hidden surfaces as design considerations. For a project review, inspect exposed and shielded areas before deciding which layout should be tested.
At the design stage, confirm where the emitters can be mounted, which way the product faces, how it moves, where sensors can observe it and how the installation can be maintained. If a surface is obscured, make that limitation visible in the trial plan rather than assuming that a controller setpoint covers the whole part.
Where the proposed design uses several heating zones, describe the task of each zone and the permitted adjustment range. Record how the heating section interacts with product movement, airflow and cooling. Do not assign one nominal emitter family a universal guarantee of uniformity or suitability.
Integration is a set of responsibilities and signals that need to work together. A heater supplier, machine builder, controls contractor and equipment owner may provide different parts of the project. Confirm the actual supply and service scope in writing; the word turnkey alone does not resolve those interfaces.
Use the following as a project discussion record. The responsible engineering team should adapt the checks and evidence to the actual equipment and destination requirements.
| Interface | What to confirm | Record needed |
|---|---|---|
| Electrical supply and heating loads | Candidate ratings, power-control arrangement, connections and available supply | Agreed electrical design and identified equipment |
| Conveyor or part handling | Product position, loading, travel or dwell, clearance and stop conditions | Layout and operating sequence used for the trial |
| Controls and measurement | Command and feedback signals, sensor locations, recipe ownership and access | Signal list, measurement method and approved recipe reference |
| Airflow, extraction and cooling | Material releases, heat removal and interactions with the proposed heating section | Assigned design responsibility and verified operating conditions |
| Access and abnormal operation | Maintenance access and the required response to a stop or loss of a supporting function | Project-specific review, checks and responsible sign-off |
Resolve these points before the production trial. A change in airflow, product spacing or handling can alter the conditions under which a heating recipe was approved. Safety and protective functions require the responsible equipment team's assessment; this checklist is not a declaration of compliance.
A useful acceptance plan identifies the product, operating conditions, measurement method, acceptance criterion and person responsible for the decision. Agree those details before collecting results. Otherwise a temperature image, a good-looking sample and an energy reading may describe different operating conditions.
Record the product temperature history at relevant locations and under representative loading. Controller output or zone percentage is a command, not proof of the temperature reached by the workpiece. Keep the sensor type, location, viewing arrangement and data collection method with the result.
If a thermal camera is used, account for calibration, emissivity and spatial resolution. NISTIR 8098 explains these measurement considerations for a particular camera procedure; it is not an oven acceptance standard. A visible surface image should not be treated as direct evidence of an unobserved interface or internal temperature.
| Acceptance item | Conditions to keep identifiable | Evidence for the decision |
|---|---|---|
| Thermal profile | Product, load, zone recipe, handling and sensor arrangement | Recorded temperature history at agreed locations |
| Product quality | Material or coating reference and conditioning or test timing | Results from the agreed process or product test |
| Production rate and repeatability | Accepted output, loading pattern, changeover and stabilization conditions | Repeated runs and the range observed |
| Energy comparison, when required | Same measurement boundary, equivalent accepted output and included auxiliaries | Measured energy and production records, with exclusions stated |
| Exceptions and release | Unmet conditions, approved deviations and further work | Documented disposition and identified approval responsibility |
These are suggested project records, not fixed numerical limits. The material, equipment and quality owners must agree the actual criteria. A component check, a process trial and a production release answer different questions and should remain identifiable in the documentation.
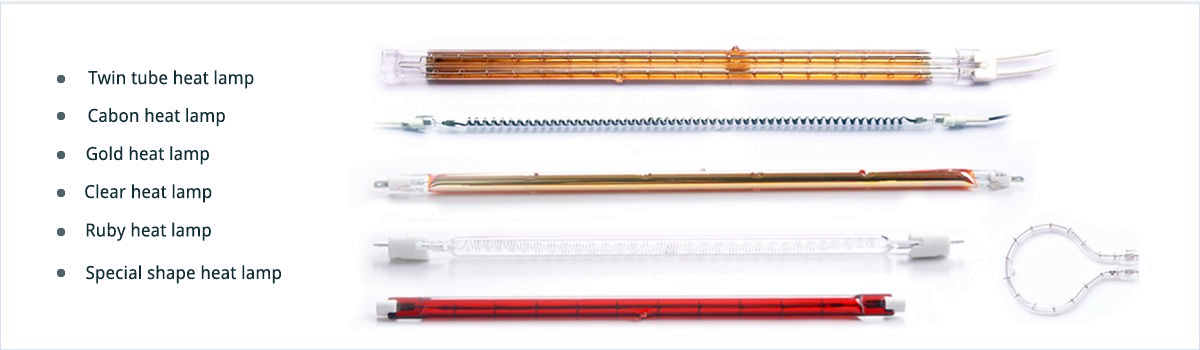
Start with the agreed installation and functional checks, then use representative workpieces to evaluate the process. Keep the product reference, heating layout, recipe and supporting conditions visible in each trial record. Change one defined factor at a time where practical so the reason for a result can be assessed.
Check more than steady production. Include the operating situations that the project requires, such as startup, product gaps, a controlled stop, restart or a format change. The required response belongs in the equipment design and trial plan; it should not be inferred from an emitter's marketing description.
Close open items before expanding the approval to routine production. If a result is unacceptable, record the affected product and condition, the evidence, the proposed adjustment and the verification required. Do not turn a successful correction on one part into a general claim about all industrial applications.
Keep the final layout, identified emitters, zone assignments, recipe, measurement method and product acceptance results together. Specify who retains the records and who can approve a later change. The same principle applies to replacement emitters: the installed part and its position must remain linked to the approved reference.
Plan inspection and cleaning around the actual equipment and contamination conditions. Reflectors, emitters, connections, ventilation and product handling are relevant review points, but maintenance intervals and replacement criteria need product-specific instructions and operating evidence. Infrared equipment should not be assumed to be maintenance-free.
When material, geometry, coating, loading or process conditions change, identify what needs rechecking. An approved recipe remains useful only when the conditions covered by its approval can still be recognized.
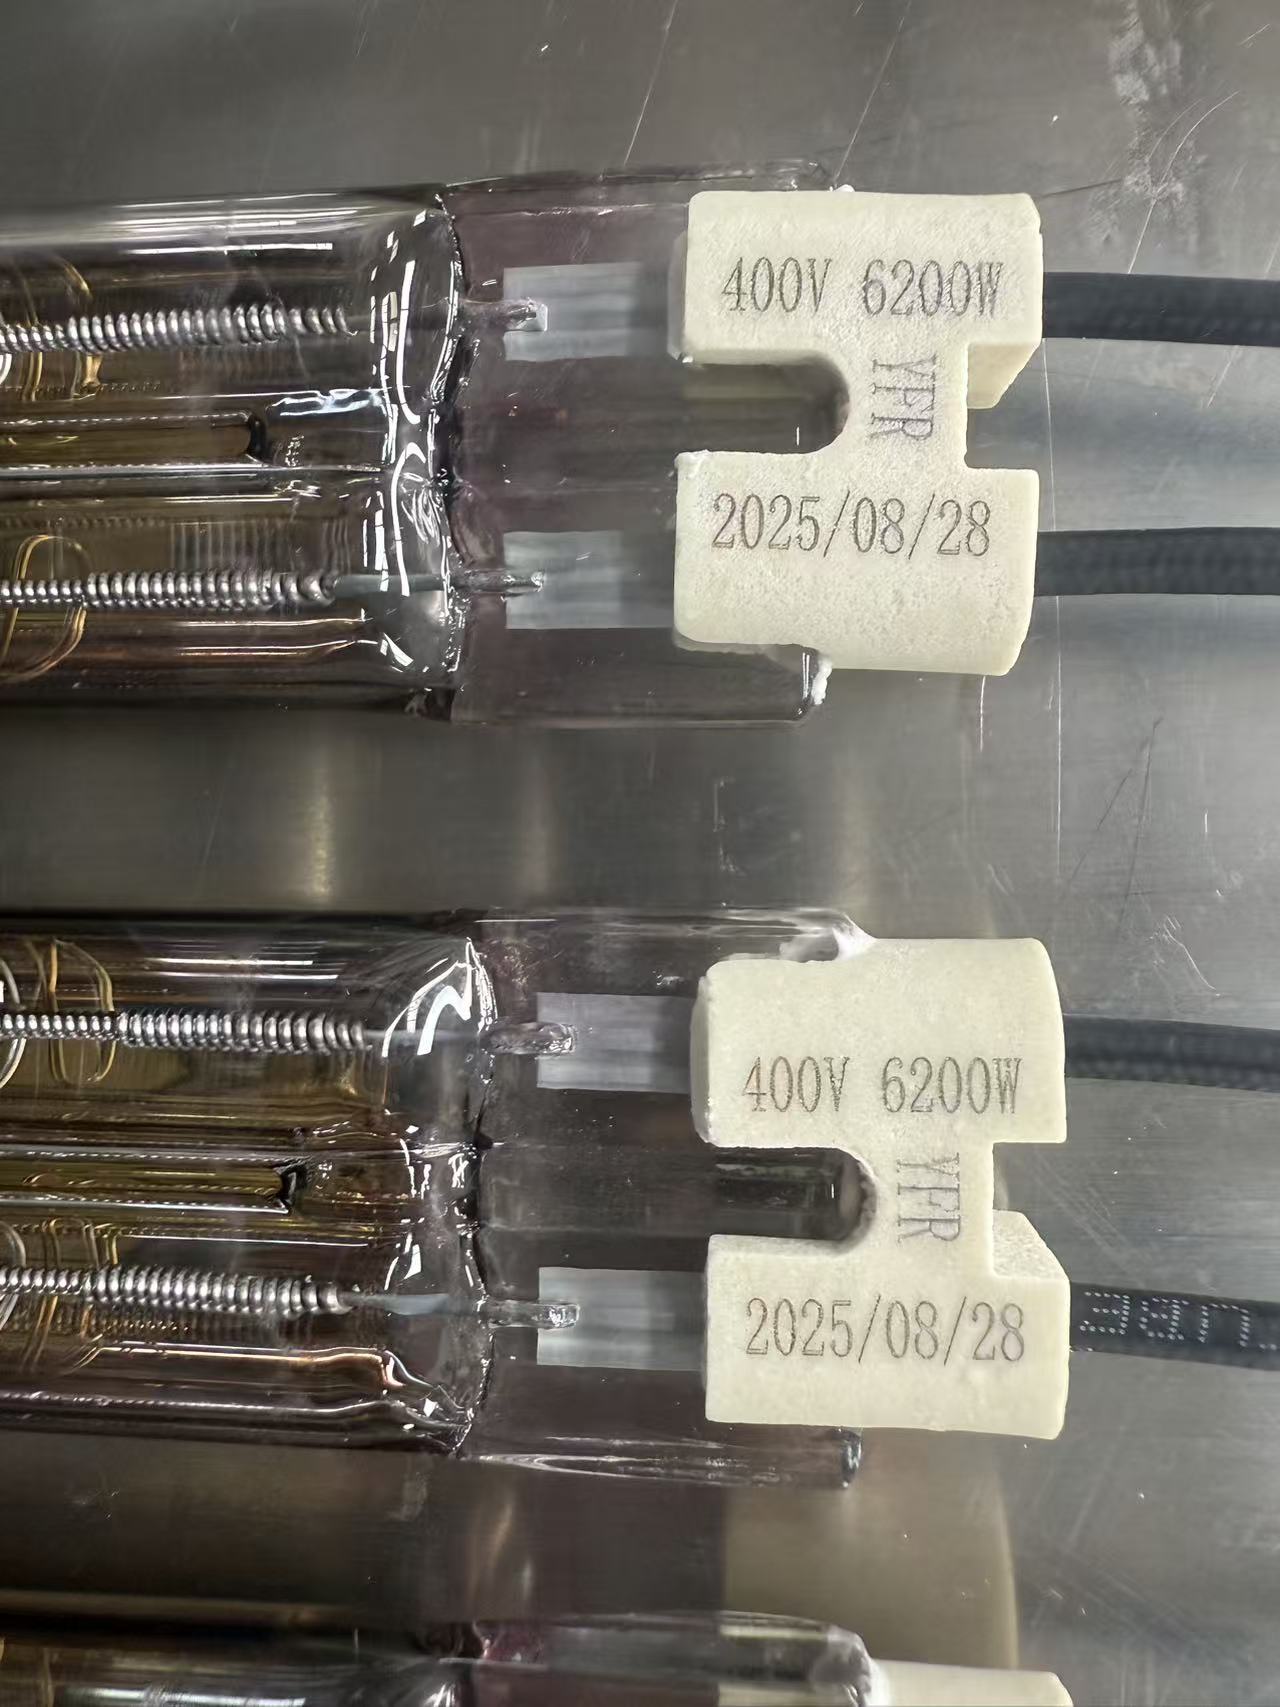
No. The result depends on the product, heating layout, controls and process conditions. Define the quality endpoint and verify it on representative workpieces; uniformity and reduced defects are outcomes to demonstrate.
Compare the product geometry, required process window, output, handling and available space with the proposed arrangement. Identify gaps before asking a supplier to confirm a custom scope.
Review the physical, electrical, control, handling and airflow interfaces first. An integration proposal should identify the work included, the responsible parties and the conditions that will be tested.
Use the equipment instructions and actual operating conditions to define access, inspection, cleaning and replacement checks. Retain the approved component references so maintenance does not introduce an unreviewed change.
Compare measured energy under equivalent product, output and quality conditions. State whether the boundary includes ventilation, cooling, handling, warm-up and interruptions. Installed wattage alone is not an energy-saving result.
Only the agreed trial scope is demonstrated. Differences in material, shape, coating, loading or acceptance requirements need review before the approval is extended.
Ask which installation, startup, documentation, training, spare-part and later support tasks are included, who performs them and what remains the buyer's responsibility. Do not infer a supplier's service scope from the word turnkey.
Send YFR the product and material reference, process objective, representative geometry, output, available space, existing equipment and known quality issue. Request confirmation of the proposed component or heating scope, assumptions and information still needed.
Review the industrial infrared heating lamps and heating modules and controls, then send the project inputs for an enquiry. Product categories are starting points for discussion, not evidence that a complete oven or service package has been approved.
DOE / IHEA Process Heating Sourcebook, Third Edition: application testing and system considerations.
NISTIR 8098: Calibration and Measurement Procedures for a High Magnification Thermal Camera: measurement-method limitations.


