Author: Site Editor Publish Time: 2025-06-12 Origin: Site
Industrial infrared lamps deliver radiant energy to a product without physical contact. They can support drying, curing, preheating and forming when the emitter and installation match the material. Their value should be judged by the resulting process quality, throughput and energy use.
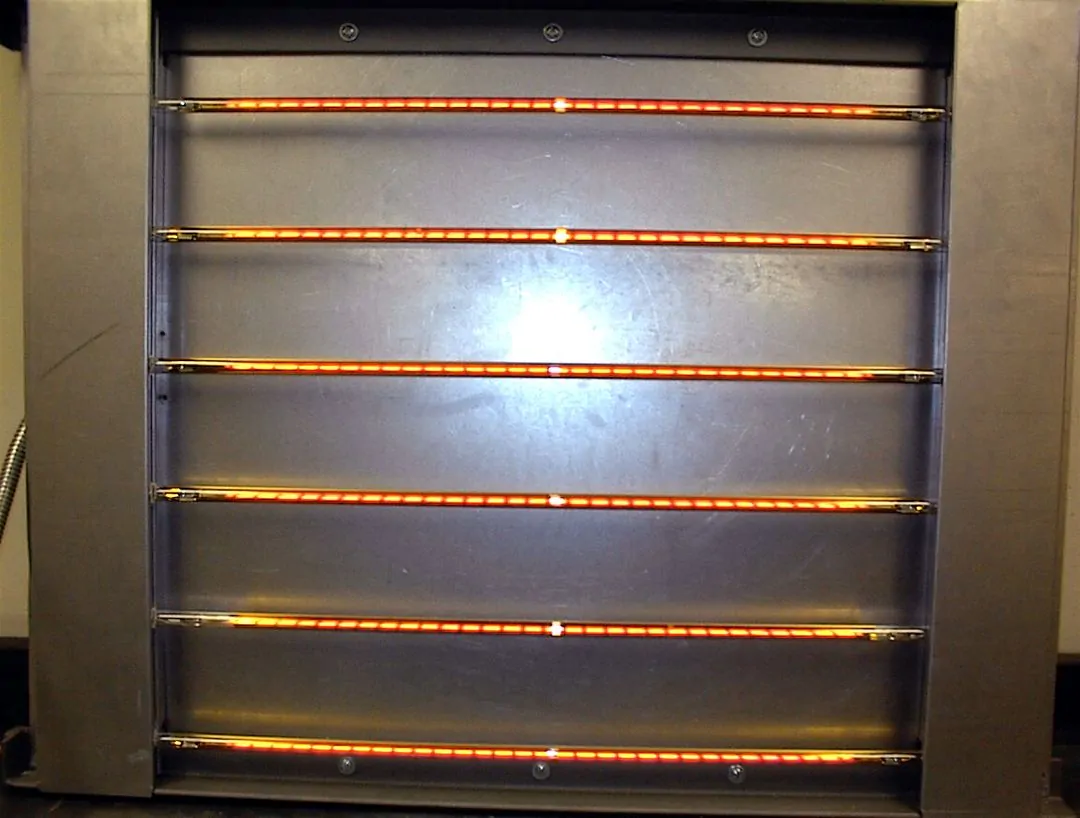
Infrared heating panel example. Process suitability and performance require validation on the actual material.
| Process | Heating objective | Key condition |
|---|---|---|
| Coatings and paint | Dry or thermally cure the specified coating | Coordinate flash-off, airflow and part temperature. |
| Printing | Assist drying of a compatible ink or coating | Check chemistry, substrate temperature and handling quality. |
| Plastics | Prepare material for forming, welding or bonding | Validate material-temperature distribution and cooled-part quality. |
| Textiles | Supply heat during drying or finishing | Control moisture removal, speed and heat-sensitive fibres. |
| Food processing | Support a defined heating or drying step | Validate food quality and any required microbial process independently. |
An infrared lamp does not itself establish sterilization, eliminate textile shrinkage or make every printed sheet ready for immediate handling. Those outcomes depend on the complete process and its acceptance tests.
Use short-wave, medium-wave and carbon infrared emitters as candidate technologies. Their response and spectrum differ, while useful heating also depends on distance, exposure, surface condition and the material’s absorption.
Medium-wave absorption is often concentrated near the surface in absorbing materials; it should not be described as automatically providing deeper penetration. Carbon construction also does not guarantee uniform heating. Lamp spacing, geometry and control determine the actual distribution.
A bare emitter is a component. A module can combine emitters with a housing, reflectors and specified interfaces, but still requires suitable machine integration. Confirm the scope of supply: supports, wiring, power controls, sensing, cooling, guards and stop-response functions are not automatically included.
For curved parts or narrow heating zones, custom geometry may be useful. Review drawings and thermal expansion, as well as access for cleaning and replacement. A shaped emitter can improve geometric coverage but still needs a material-temperature test.
Coordinate lamp power with line speed or the machine cycle. Use a measurement method appropriate to the surface and the required temperature location. Define permitted variation across the part and examine hot spots, shadowed regions and cold starts.
The systems and controls selection should include the normal operating cycle and the response to a stopped line, loss of airflow or sensor fault.
Compare accepted throughput and energy per accepted part at the same quality requirement. Include exhaust, fans, cooling, idle time and rejected material when relevant. A nominal lamp efficiency or a successful application elsewhere is not a guaranteed saving for a new installation.
For an existing oven, document the current lamp layout, cycle and product-temperature history before making changes. Record lamp identification and positions so that a replacement can preserve the validated arrangement.
Only if the specific supplied system and application are designed for that use. Confirm interfaces and integration responsibilities.
No. Excess power may damage the product or exceed electrical and cooling limits.
Material, geometry, throughput, required thermal profile, installation space and electrical supply.
Measure complete process energy against a comparable baseline and report the quality and throughput conditions.
Send the process, material, heated area and current equipment data for an infrared system review.
Last updated: September 7, 2026


