Author: Process Heating Engineer Publish Time: 2026-03-27 Origin: Site
Last updated: October 16, 2026
When comparing infrared drying vs hot air drying for printing, start with the ink or coating's drying mechanism. For an evaporative system, two questions matter together: how energy reaches the wet layer, and how evaporated water or solvent leaves that layer and the drying zone. Infrared can be a candidate for radiant heat input; hot air supplies convective heat and supports vapor transport. Neither method can be selected from the speed target alone.
A dryer can look powerful on paper and still underperform if it heats the web without adequate vapor removal, or moves air without delivering enough usable heat within the available exposure. Establish the measured limit before specifying an IR, hot-air or hybrid change.
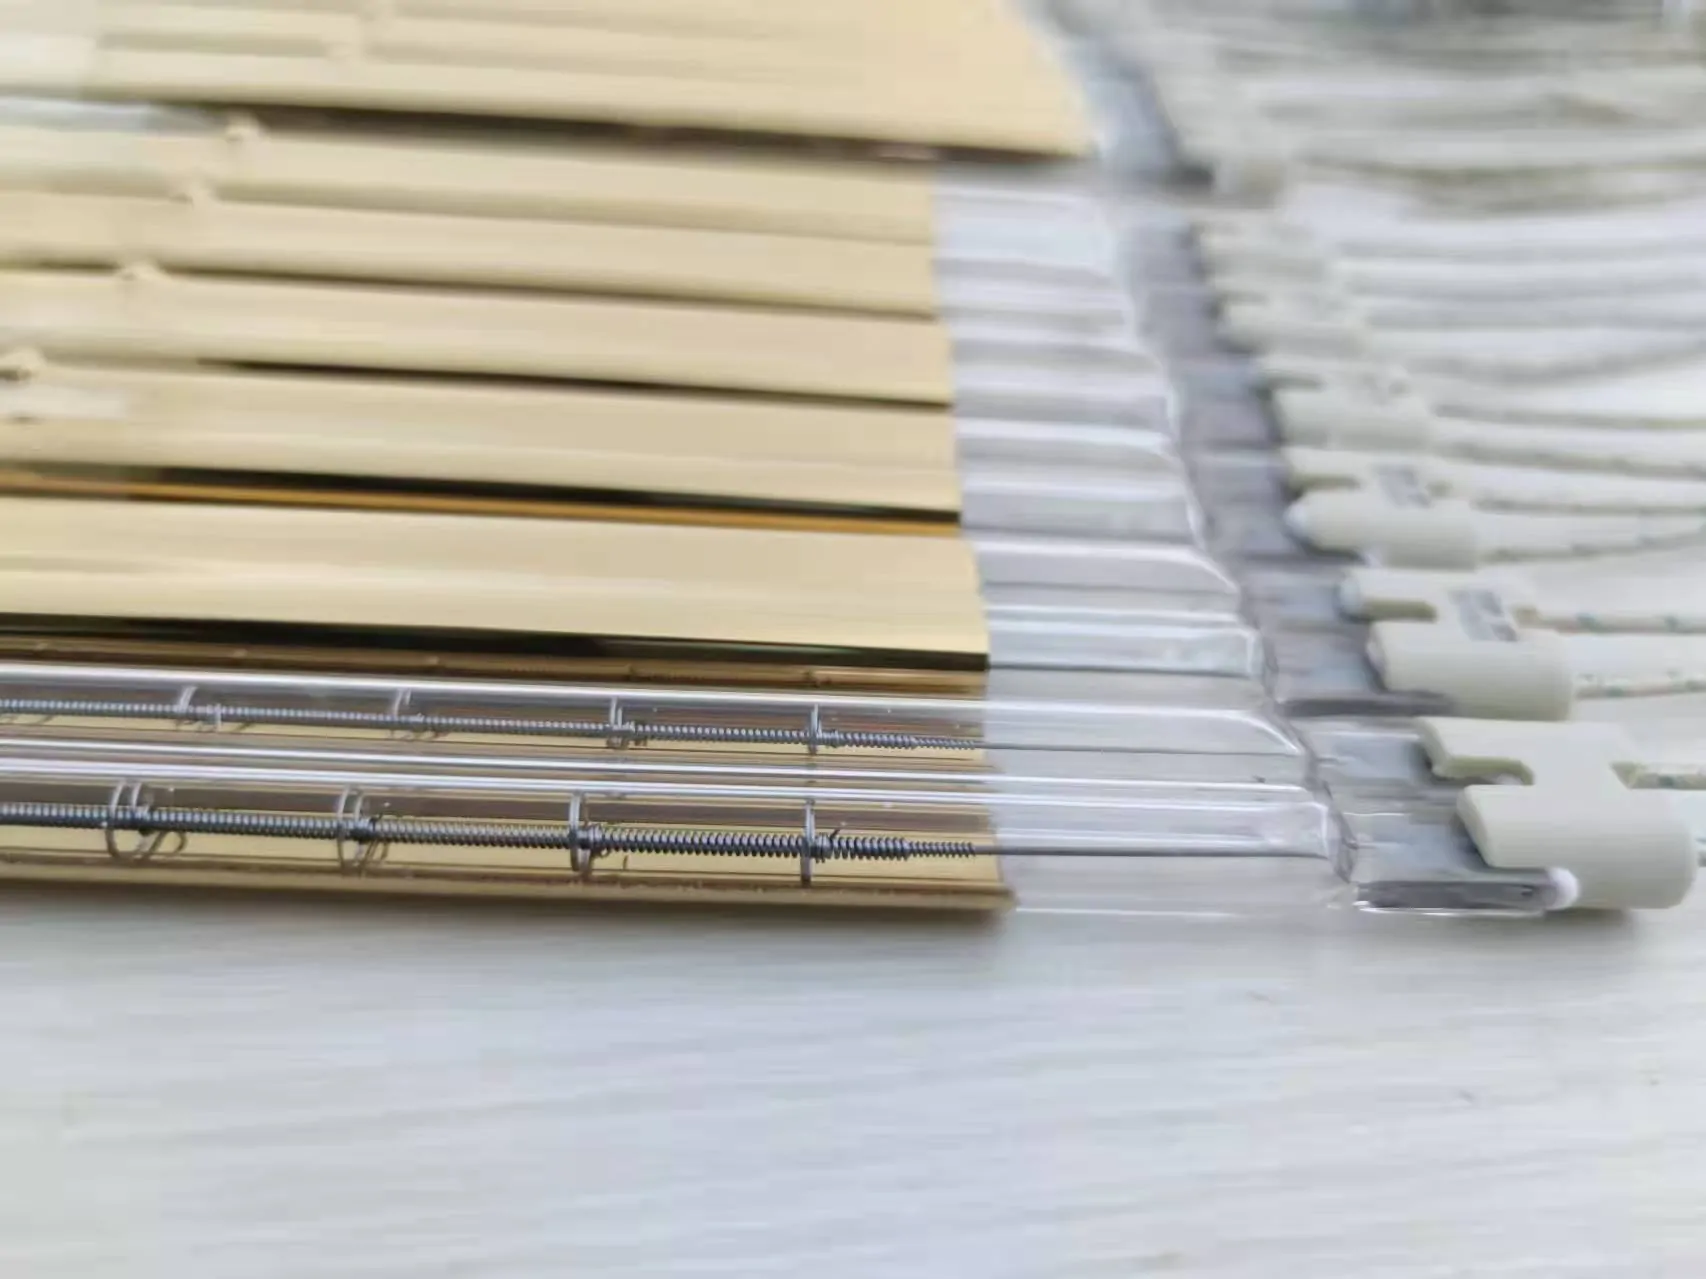
Water-based and solvent-based evaporative inks need the relevant liquid to leave the printed layer. Heatset offset inks involve evaporation of ink oils. Traditional non-heatset offset inks can instead set and dry through absorption and/or oxidation. UV- or electron-beam-curable inks require the energy and conditions specified for their reactive cure. Adding infrared heat is not a substitute for a specified UV or EB curing process.
The U.S. EPA's printing-facility technical guidance describes these different mechanisms in its printing-process background. The distinction matters here as a starting classification; the formulation supplier's current instructions define the actual drying or cure requirements. Other reactive or mixed-mechanism systems also need their own process conditions.
The heat-and-vapor-removal comparison below mainly concerns evaporative printing inks and coatings. A dry-to-touch surface, absorption into paper and a completed chemical cure are different outcomes. Identify the acceptance test needed before treating any of them as a successful drying result.
Infrared is a candidate when the printed layer needs additional useful heat within the available exposure. The U.S. DOE process-heating sourcebook explains that absorbed radiation heats the material and recommends application testing. It also emphasizes appropriate controls. This supports evaluating a radiant option; it does not predict the speed gain or footprint of a particular printing retrofit.
If the line cannot be extended, review whether a proposed radiant zone can fit the machine and deliver the required result. Include mounting space, shielding, access, cooling where required and the existing air-handling arrangement. The available installation envelope includes more than the lamp length.
An incompletely dried web does not, by itself, prove a heat-input shortage. Compare the product temperature profile, ink loading, dwell time and air-side conditions at a good operating point and at the problem speed. If inadequate thermal input remains a supported hypothesis, a controlled trial can test additional radiant or convective input without exceeding the substrate's process limits.
For evaporative systems, air movement near the web and removal of vapor from the dryer are part of the process. Hot air can supply heat as well as carry vapor away from the surface. Recirculation, fresh air and exhaust have different roles; increasing one setting does not necessarily correct the whole air-side balance.
This is why some presses do not respond well to more IR alone. If the surface heats rapidly but vapor removal is inadequate, the operating window can narrow without an acceptable dry-down result. More surface temperature is not the same as less residual liquid.
Check air distribution, obstructions, filter and nozzle condition, exhaust balance and the conditions of air entering or recirculating through the zone. Review water-vapor loading or solvent-handling requirements as appropriate to the formulation and dryer instructions. Do not reduce exhaust or bypass a machine interlock to compensate for an unsuccessful heating trial.
A faster dryer is not automatically a better dryer. A trial that improves apparent surface dryness can still introduce problems if heat input is too aggressive for the substrate, coating structure or downstream operation.
Define the relevant quality checks for the job: for example, set-off or blocking at the next handling stage, adhesion or rub performance where specified, and dimensional or visible changes. For paper-based jobs, register, flatness and later folding may matter. Films and coated webs may have different limits. These are checks to agree for the actual material, not defects that every dryer will cause.
The target is stable drying at the required speed without pushing the paper, film, or coating beyond its agreed process window. Check dry-down quality, dimensional behavior and repeatability during ramp-up and ramp-down, as well as steady production. Keep the evaluation interval consistent when comparing samples after drying.
The narrower the substrate's temperature margin, the more valuable controlled exposure, zoning and reliable measurement become. Confirm where temperature is measured and whether that reading represents the surface or layer that limits the process.
Assess the hottest and least-treated areas, product variation and the result at the next printing or finishing stage. A hybrid arrangement is one candidate when radiant input and air-side work are both needed. It still needs a trial; combining technologies does not automatically provide a wider process window or better uniformity.
Printing lines do not run in one perfect steady state. They accelerate, pause, recover, and change jobs. Compare the installed response of the proposed emitter, controller and sensing arrangement, rather than assigning one response time to all infrared heaters. Include retained heat after output is reduced and the web's exposure during a stop.
For a hot-air zone, review air temperature, distribution, circulation and exhaust behavior through the same transitions. Agree on the machine's speed-linked settings, shutdown sequence and interlocks with the responsible equipment team. An unstable transition may involve heating, airflow, controls or the ink application; it is not sufficient evidence to prescribe a faster lamp alone.
This table is a practical comparison for evaporative inks and coatings. The entries describe roles and checks, not guaranteed advantages for every design.
Comparison point | Infrared drying | Hot air drying |
|---|---|---|
Primary role | Radiant heat input, where the product absorbs it usefully | Convective heat input and air-side vapor transport |
When to evaluate | A supported need for additional or differently distributed heat input | A supported need for convective input, air distribution or vapor-removal improvement |
Response speed | Measure the proposed emitter and installed control response | Measure the proposed zone's thermal and air-handling response |
Installation space | Check the complete module envelope, clearances and integration | Check the zone, ducts, circulation and exhaust requirements |
Substrate risk | Excess local loading or exposure can overheat the product | Air temperature, distribution and exposure can also exceed product limits |
Control focus | Emitter zoning, output, web distance, exposure time and product feedback | Air temperature, flow pattern, recirculation, fresh air and exhaust balance |
Common mismatch | Adds heat while leaving a vapor-removal limit unresolved | Changes airflow without correcting inadequate useful heat input |
Candidate retrofit role | Test a radiant contribution within the verified product window | Test the required convective and air-side changes within that window |
This is an illustrative scenario, not a YFR customer case or a performance forecast. Assume a water-based flexo line is trying to increase speed, but the plant has little room to extend the dryer. At current settings, the web looks acceptable in steady production; during acceleration, drying becomes inconsistent.
Those symptoms leave several possibilities open. Record the wet application, product temperature, exposure time, air-side conditions and agreed dry-down result at the acceptable speed and the target condition. If the evidence supports insufficient useful heat input, compare a controlled additional-heating trial. Infrared may be one candidate, alongside the available convective changes.
Now suppose the records instead show that vapor handling deteriorates as evaporative load rises, while product temperature is already approaching its limit. Investigate airflow and exhaust performance before adding heat. If both limits are supported, evaluate the combined changes. No speed gain, energy saving or equipment choice follows from the scenario alone.
Use the observations to define a hypothesis and a check. Similar symptoms can have different causes, so the table is a starting point for diagnosis rather than an equipment prescription.
What you observe on press | Hypothesis to check | Evidence or trial to consider |
|---|---|---|
Speed rises with fixed dryer length and drying becomes incomplete | Insufficient useful heat or vapor-removal capacity at the shorter exposure | Compare temperature, application loading, air-side conditions and dry-down at both speeds |
Surface heats quickly but dry-down improves little | A vapor-removal limit, unsuitable heat distribution or a different drying mechanism | Confirm ink chemistry; check air-side performance and the specified acceptance test |
Quality becomes unstable during acceleration or job changes | Response, settings, loading or synchronization mismatch | Record the transition and test coordinated settings with the equipment team |
Drying is uneven across the width or changes with load | Nonuniform air or radiant input, or variation in wet application | Map the product result, application and heating conditions across the width |
The substrate approaches its temperature limit | Heat is being added outside the useful product window | Review distribution, exposure, measurement and air-side capacity before raising output |
There is no room for a long dryer extension | An installation constraint, with the process limit still to establish | Measure the full envelope and compare feasible options against the same product test |
Substrate type, thickness and relevant product limits.
Ink or coating chemistry, supplier instructions and required drying or cure mechanism.
Wet application or coating weight where known, and representative job variation.
Current and target line speeds, heated length and exposure time.
Existing dryer type, zone layout and complete installation-space limits.
Air distribution, recirculation, fresh-air and exhaust arrangements.
Measured product temperatures and air-side conditions at good and problematic settings.
Where the process becomes unstable: startup, ramp-up, steady run or shutdown.
Acceptance tests for dry-down, set-off, blocking or other job-specific requirements.
Controller, sensor and interlock information relevant to any proposed change.
No. A useful speed increase depends on the ink mechanism, product response, available exposure and vapor removal. Compare specific designs using the same product and acceptance tests.
When measurements support a problem with convective input, distribution or vapor handling. An incomplete dry-down result alone does not identify which air-side setting needs to change.
Yes. Excess output or exposure can exceed the product window. Review zoning, distance, sensing and stop behavior for the actual installation; hot-air settings also need product limits.
It is one way to combine radiant input with convective heating and vapor transport where those roles are needed. Confirm the combination through trials rather than assuming that it outperforms either method alone.
No. Follow the ink supplier's specified cure mechanism and equipment conditions. A warm or dry-feeling surface is not proof of a completed reactive cure.
For an infrared lamp enquiry, share the substrate, ink system, speed, available space, temperature limits, current dryer and the observed problem. Include existing lamp and control data where available. These inputs help define what a candidate lamp specification must address and which machine or formulation questions remain with the relevant equipment and ink suppliers.
Send YFR your printing application details and confirm the scope of any proposed supply or technical review. A lamp enquiry does not, by itself, establish a complete dryer retrofit design.


