Author: Site Editor Publish Time: 2025-08-09 Origin: Site
Last updated: October 15, 2026
Uneven heating, slow drying and recurring hot spots are useful starting points for reviewing an industrial infrared process. They do not identify a lamp specification by themselves. A practical review connects the product defect with the material, the temperature history, the heater arrangement and the operating conditions.
For a coating line, plastic component or other manufactured part, first define what an acceptable result looks like. Then collect enough information to distinguish a heating problem from a material, handling or measurement problem. The following checks help prepare that discussion before a lamp, reflector or control change is selected.
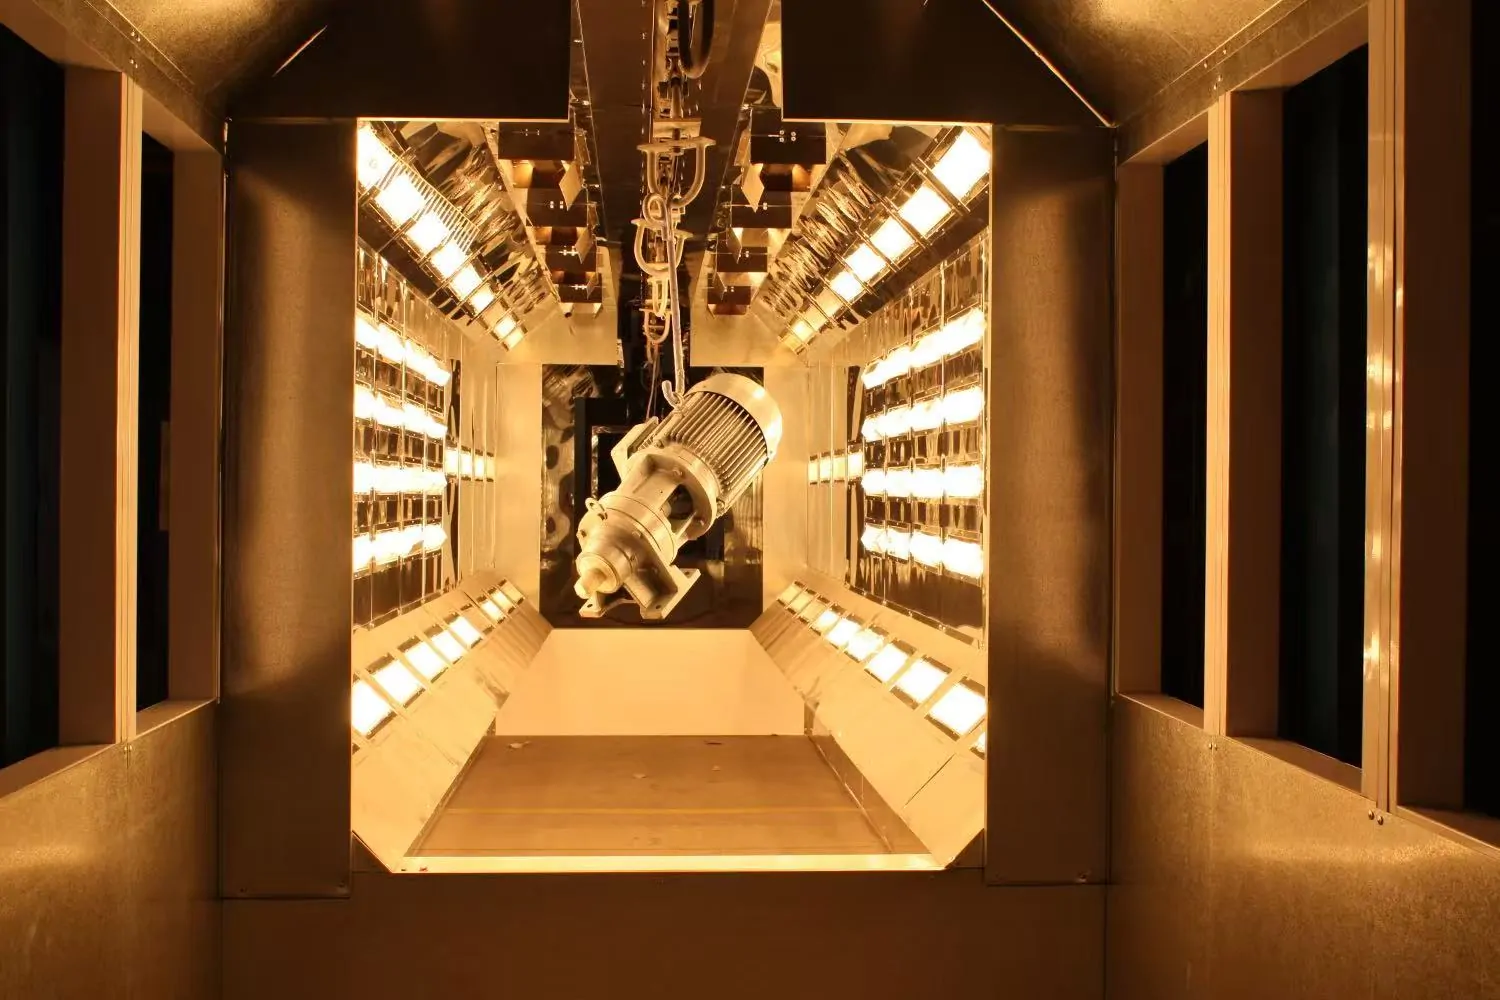
Write down the operation: preheating, moisture removal, coating drying, curing or another defined step. Include the material grade, part thickness, surface condition and the process specification that governs acceptance. A coating supplier's technical data and the equipment instructions should remain part of the review.
Record the required product temperature and time conditions, together with the permitted limits. Keep these separate from the heater setting, oven-air reading and controller output. A setpoint alone does not describe the temperature history of every part.
Identify where and how temperature is measured. Record the sensor type, target area, viewing position and measurement timing. For an infrared instrument, include the emissivity setting and the surrounding hot surfaces. NIST's thermography work accounts for both surface emission and reflected radiation; a changing reading therefore needs a measurement check before it is treated as a changing process.
Use the same documented method when comparing acceptable and rejected parts. If the instrument cannot resolve the relevant surface or the reading is uncertain, have the measurement method reviewed before using it to change the recipe.
Map the defect to its position on the part and its position in the heating zone. Note whether it appears on every part, one product family, one side of the conveyor or only after a stop. The table identifies checks to investigate, rather than diagnoses that can be made from appearance alone.
| Observed symptom | Evidence to collect | Review before changing the lamp |
|---|---|---|
| One edge or recessed area stays cooler | Temperature map, part orientation and fixture photographs | Emitter coverage, reflector condition and obstructions |
| Drying remains slow | Temperature history, wet-film or moisture condition and residence time | Material specification, airflow or exhaust conditions and the heating stage |
| A local area overheats | Defect location, heater spacing and zone settings | Local exposure, part geometry and control response |
| Results change after a line stop | Stop duration, restart sequence and controller trend | Standby settings, restart timing and interlocks |
| Performance changes after replacement | Old and new lamp identification, drawings and operating records | Electrical rating, heated length, orientation and installation details |
Inspect the arrangement from the product's position. Photograph the emitters, reflectors, holders and fixtures with the equipment safely isolated. Mark areas that are hidden or receive different exposure as the part moves.
The U.S. Department of Energy describes infrared heating in terms of absorption, emitter and reflector arrangement, and controls. For complex parts, its guidance also considers part movement and combined heating methods. Increasing the whole zone's output should therefore follow a review of the cold area's exposure and the temperature of areas already within specification.
Record the condition entering the heater as well as the condition leaving it. Include coating or adhesive identification, applied thickness where relevant, initial moisture, material temperature and the approved quality test. Clarify whether the complaint is residual moisture, tack, appearance or failure of a specified cure test.
Also record airflow and exhaust settings where they form part of the process. Review the required flash-off, heating and holding stages with the material supplier or process owner. A surface that feels dry is not sufficient evidence that every specified process requirement has been met.
Preserve the controller trend, operating recipe and photographs before adjusting settings. Compare product position, loading pattern and line speed with a known acceptable run. Check whether a hot spot follows a fixed machine position or follows the part when its orientation changes.
Keep the operating limits and the equipment's protective functions in force during the investigation. Electrical measurements and work inside the heater assembly belong to qualified personnel using the equipment's isolation procedures.
Define a trial before changing emitter type, reflector arrangement, zone output or residence time. Retain an acceptable reference part and a record of the original recipe. Select the measurements and quality tests that will determine whether the change is useful.
Choose representative parts, including the geometry or finish associated with the defect.
Record the starting material condition and the complete operating recipe.
Change one planned variable where practical, keeping a record of any unavoidable changes.
Compare product temperature history and the specified quality result.
Check normal production, a planned stop and restart, and relevant product variations before approving the recipe.
State what remains untested. A result for one material, surface finish or loading arrangement should not be presented as proof for every product on the line. For the relationship between emitters, sensors and control zones, see the industrial infrared heating system and controls guide.
A useful request describes the problem and supplies the information needed to assess it. Send original documents or clearly labelled measurements where available. Mark an unknown field as unknown instead of estimating a specification from the lamp's appearance.
| Information group | What to provide | Purpose |
|---|---|---|
| Product and material | Material grade, dimensions, surface or coating details and relevant technical data | Define the heating task and acceptance limits |
| Operating process | Line speed or cycle, loading pattern, temperature records and stop sequence | Describe actual exposure and process variation |
| Existing heater | Lamp code, rated voltage and power, drawing, heated length and photographs | Identify the installed component |
| Installation and control | Emitter layout, working distance, reflector, mounting, sensor and controller details | Review how the component operates in the system |
| Problem and acceptance | Defect photographs, affected positions, recent changes and required quality test | Agree on the investigation and trial criteria |
A broken tube, damaged terminal or repeated failure in one machine position needs a component and installation investigation. Preserve the lamp identification, failure location and photographs before safe removal. Use the separate infrared tube failure analysis and troubleshooting checklist for that evidence. This process review does not replace electrical fault finding or a failure assessment.
Should I increase lamp power when drying is slow?
First compare the product's temperature history and quality result with its process specification. Include the entering material condition, residence time and relevant airflow settings. Select a power change only as part of an agreed trial within the equipment's limits.
Does uneven colour prove that the heating is uneven?
No. Preserve photographs and compare them with measurements and the material's quality criteria. Investigate the coating or material condition as well as the heater arrangement before assigning a cause.
Can one successful trial cover all materials on the line?
Document which grades, dimensions, finishes and loading conditions were tested. Any additional operating conditions need a defined review before they are included in the approved recipe.
What should I send if the original lamp code is missing?
Send clear lamp and installation photographs, the machine identification, available electrical ratings and a dimensioned drawing. Identify uncertain details explicitly. A visual resemblance alone is insufficient to confirm a replacement.
For an application or replacement enquiry, send YFR the process details and RFQ information, including the observed symptom, existing lamp identification and acceptance requirement. The proposed lamp specification, installation conditions and trial scope should be confirmed before an order or process change.
U.S. Department of Energy: Process Heating Sourcebook, Third Edition — electric infrared processing and system review.
NIST: Calibration and Measurement Procedures for a High Magnification Thermal Camera — measurement principles and emissivity.


