Author: Site Editor Publish Time: 2025-09-15 Origin: Site
No. Infrared paint curing does not affect all materials equally. The coating absorbs part of the radiation, the substrate may absorb or transmit another part, and heat then redistributes through the assembly. The same lamp setting can produce different temperatures on different colours, thicknesses and shapes.
Evaluate the complete coating–substrate combination. A material that tolerates heat can still carry a coating, adhesive, insert or seal with a lower temperature limit. A surface temperature reading alone does not prove complete cure through the film.
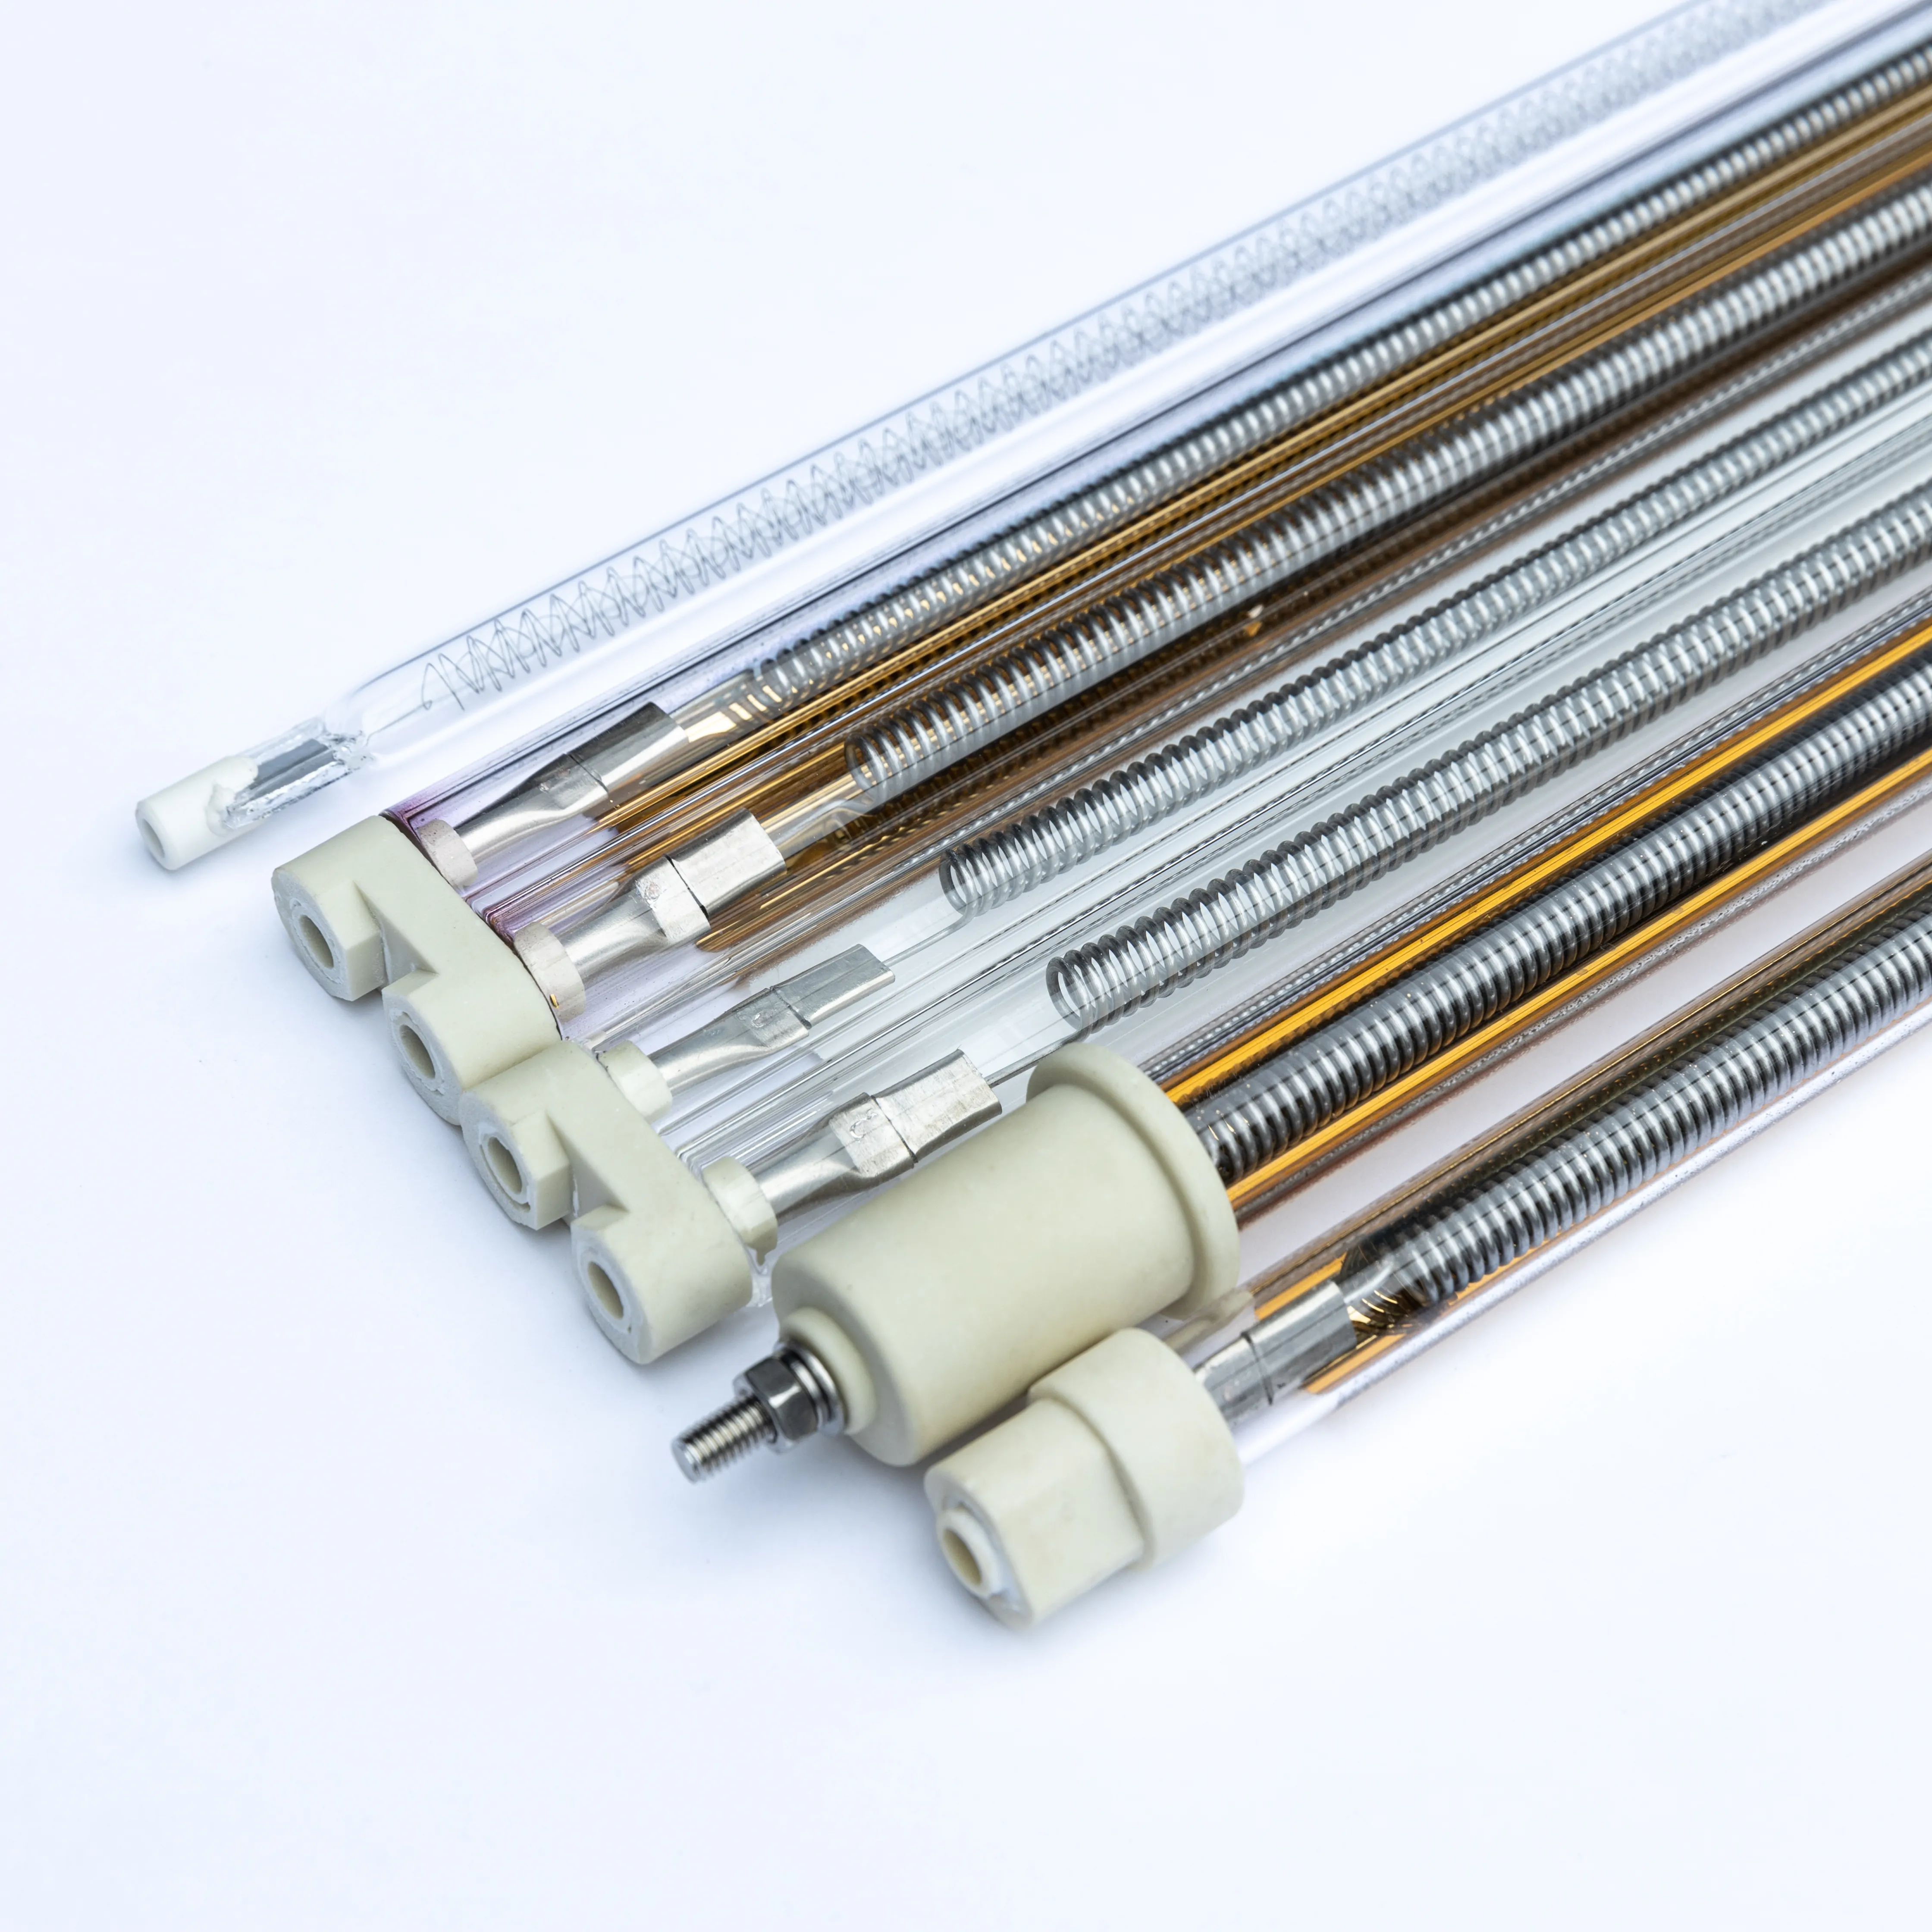
Product examples; the pictured lamps do not establish a cure schedule for any particular material.
| Material | Main process concern | Useful validation |
|---|---|---|
| Metal | Heat spreading, reflective surfaces and variation in section thickness | Check hot and cold positions using a suitable temperature measurement method. |
| Plastic | Softening, warping and effects of pigment or filler | Test dimensional stability and coating adhesion on the actual grade. |
| Wood | Moisture movement, resin effects and uneven surface heating | Check moisture condition, finish and dimensional change after cooling. |
| Composite | Different layers, fibres, resin and bonded components | Confirm each constituent’s thermal limits and inspect the complete assembly. |
| Glass or ceramic | Thermal gradients and coating-specific cure requirements | Use a controlled ramp and check adhesion and thermal-stress damage. |
Emitter spectrum influences where radiation is absorbed, but heating depends on power, distance, exposure time and part geometry as well. Heat absorption should not be confused with thermal conductivity. A material can absorb radiation strongly while conducting heat slowly, creating a hot surface over a cooler interior.
Drying removes volatile components; thermal curing develops the properties of a heat-reactive coating. UV curing requires the appropriate photochemistry and light source. Findings about reflective or cooling coatings cannot be used as evidence that infrared heating cures paint at a lower temperature.
Lamp family names describe useful starting options, not an automatic material match. Test the actual finish and substrate with the proposed emitter. Compare short-wave and medium-wave infrared lamps using the same accepted cure requirement.
Confirm film thickness, mixing and induction requirements, flash-off, allowed part temperature and hold time. Follow the specified temperature definition and measurement location.
Include edges, recesses, thick sections, dark areas and positions shadowed by fixtures. Check both overheating and under-curing rather than accepting the average temperature.
Use the coating supplier’s adhesion, hardness, appearance and cure checks after the prescribed cooling or conditioning period. A tack-free surface alone is insufficient.
Changing the substrate thickness changes its thermal mass. Changing paint colour can change absorption. A reflective fixture may create a local hot spot. Switching from a flat panel to a shaped component changes exposure and shadowing. These changes require verification even when the lamp, wattage and timer remain the same.
Airflow must remove released moisture or solvent while preserving the coating’s required process conditions. A rapid temperature rise may trap volatiles or damage heat-sensitive layers. The paint-drying process control guide covers flash-off and defect checks in more detail.
No. Any emitter can overheat a plastic if absorbed energy exceeds its process limit.
Not directly. Part temperature depends on absorbed energy and heat losses over time.
Only after tests show that the intended colour and material range meets the same cure and temperature requirements.
Compare complete process energy per accepted part under equivalent coating thickness and quality criteria.
Last updated: September 7, 2026


