Author: Site Editor Publish Time: 2025-09-18 Origin: Site
Last updated: October 18, 2026
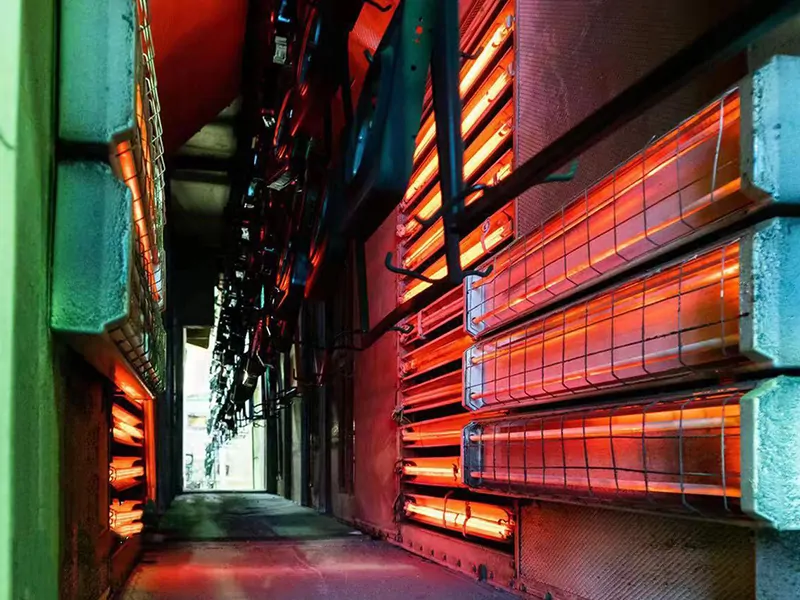
On a continuous coating line, infrared drying requires a controlled thermal recipe. Good results depend on preparation, application consistency, radiant coverage, vapour removal, temperature feedback and a clearly defined acceptance test. This workflow follows the wet coating from application through the heating zone to release inspection.
Record coating type, solids or solvent system, wet and dry film build, flash-off requirement, target temperature, hold time and final quality test. Use the coating supplier’s current technical data as the primary process limit.
Surface cleanliness, pretreatment and film uniformity affect both adhesion and drying. If the coating thickness changes across the part, the required energy and vapour-release rate will also change. Record the incoming wet-film build and the line speed together so a trial can be repeated with the same coating load and exposure.
| Parameter | Purpose | Production check |
|---|---|---|
| Emitter waveband | Influences absorption and response | Trial against the real coating and substrate |
| Working distance | Changes irradiance and coverage | Measure from emitter to the actual surface |
| Power and zoning | Controls heating rate and uniformity | Record each zone setting |
| Exposure time | Sets the delivered thermal dose | Link to conveyor speed or cycle time |
| Reflector condition | Directs energy toward the work | Keep clean and inspect for damage |
Radiant heat can accelerate evaporation, but released moisture or solvent must still leave the surface and enclosure. Airflow should remove vapour without disturbing the coating, cooling one side excessively or creating dust defects. Hazardous atmospheres require an engineered safety review. Noblelight’s Infradry documentation provides a concrete example of IR heating combined with warm air and extraction for water-based coatings; radiant energy and vapour removal remain separate design duties.
Use suitable temperature measurement and locate the sensor where it represents the critical surface. Emissivity, viewing angle and reflective surfaces can affect non-contact readings, so measurement should be checked against the application.
Confirm the coating with the specified appearance, adhesion, hardness, solvent-resistance or moisture test. Record defects such as blistering, pinholes, colour shift, undercure and edge overheating, then adjust one variable at a time.
Validate the full range of part sizes, colours, line speeds, starts and stops. Have the line integrator define and test the heater response to a conveyor stop, loss of extraction and overtemperature before release. Noblelight’s wet-coating guidance describes shutting down suitably responsive emitters during conveyor stops; the response must be verified for the installed emitter and complete line. A successful laboratory result is only the beginning of production qualification.
Compare YFR infrared heating lamps, heating systems and controls and infrared application cases when planning a new zone or retrofit.
Heating depth depends on coating and substrate absorption. The process must be validated for the complete film and required cure result.
Not necessarily. Excess heating can trap volatiles, overheat the substrate or reduce uniformity.
Airflow and exhaust help remove released vapour and stabilize the process environment.
Record material, coating, film build, lamp settings, distance, speed, airflow, measured temperature and the final quality result.
Send YFR your coating data, part dimensions, cycle time and available installation space for a focused application review.
General infrared process-heating guidance: U.S. Department of Energy process-heating sourcebook.


